What Are the Top Types of Threaded Inserts?

Threaded inserts add durable internal threads to materials that may be too soft, thin, or fragile for repeated screw fastening. They are common in plastics, wood, composites, and light-metal assemblies. Small parts. Big consequences. A poorly matched insert can spin, loosen, or damage the surrounding material during installation or service. The phrase “Inserts Threaded” covers a broad family of components, not one universal solution. Each design works differently, and performance depends on the base material, hole size, installation method, and expected load.

Common types include heat-set inserts for thermoplastics, press-in inserts for prepared holes, ultrasonic inserts for controlled plastic assembly, and self-tapping inserts that form their own threads. Screw-in inserts are often used in wood, while key-locking styles can resist rotation in demanding applications. These categories overlap in purpose, but they are not interchangeable. A neat catalog description can still hide a poor fit. That deserves a second look.

This guide compares the main insert types, their installation requirements, and practical strengths and limitations. It also highlights details worth checking, such as wall thickness, pilot-hole diameter, pull-out resistance, and access for installation tools. For example, a heat-set insert needs suitable temperature control and placement; a press-in style needs a correctly sized hole. Choosing carefully helps prevent stripped threads and costly rework. There is no perfect insert. The reliable choice is the one tested with the actual material, fastener, and assembly conditions.
What Are the Top Types of Threaded Inserts?

What Threaded Inserts Are and How They Create Reusable Threads

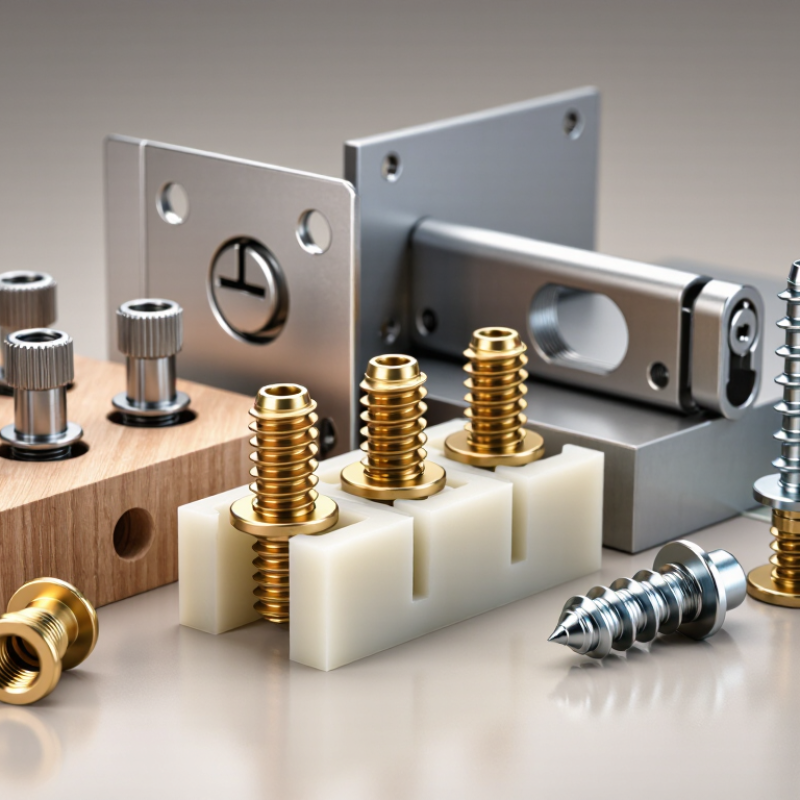
Threaded inserts are components installed in a prepared hole to provide an internal thread for a screw or bolt. They are useful when the surrounding material is too soft, thin, or worn to hold repeated fastener changes reliably. Some inserts are solid sleeves; others use a helical wire coil. Press-in and heat-set designs are also common for plastic parts.

The insert’s outer surface grips or bonds with the base material, while its inner thread accepts the fastener. This creates a more durable contact point and can help spread tightening forces across a larger area. Reuse still depends on correct installation, material strength, and the load applied.

Fit comes first. A hole that is too large may let an insert loosen; one that is too small can distort the part. I would check the manufacturer’s sizing guidance rather than assume all inserts use the same drill size.

For example, a heat-set insert in a plastic panel needs controlled heat and steady pressure, while a wire insert typically requires a tapped hole and careful alignment.

Even a well-made insert can fail if the surrounding material cracks. That detail is easy to miss.
How Threaded Inserts Are Classified by Installation Method

What Are the Top Types of Threaded Inserts?
How Threaded Inserts Are Classified by Installation Method

Threaded inserts are often grouped by how they enter and lock into a workpiece. Press-in inserts use knurls or ridges to grip a prepared hole. They suit firm materials, but a hole that is too large can weaken the fit. Heat-set inserts soften surrounding thermoplastic during installation, then hold as it cools. Ultrasonic inserts use vibration to achieve a similar result. The equipment and heat control differ. Molded-in inserts are placed in a mold before plastic is formed around them, creating a strong mechanical anchor.

Screw-in inserts cut or engage their own path in wood or plastic, or fit into a prepared threaded hole. They can be useful for repairs and assemblies that may need repeated fastening. Blind-installed inserts, including rivet nuts, are set by pulling a tool from one side of sheet material. They work where the back face is inaccessible. That matters. Each method depends on material thickness, hole tolerance, expected load, and available tools. Real results can vary; even a well-chosen insert may loosen if installation is misaligned.

Tips: Test the insert in a sample piece first. Check hole diameter, insertion depth, and alignment. For plastics, avoid excessive heat or force, which can deform the surrounding material.

What Are the Top Types of Threaded Inserts? — How Threaded Inserts Are Classified by Installation Method
Insert Type Installation Method Common Materials or Workpieces Typical Advantages Key Considerations
Heat-Set Inserts A heated installation tip softens the surrounding thermoplastic as the insert is pressed into a prepared hole. The plastic flows around the insert and solidifies as it cools. Thermoplastic parts, including many 3D-printed components Can provide durable metal threads and good resistance to pull-out and rotation when correctly installed. Hole size, insert geometry, temperature, and installation depth must suit the plastic and insert. Excessive heat or pressure can damage the part.
Ultrasonic Inserts Ultrasonic vibration and pressure generate localized heat, allowing the insert to embed into a prepared thermoplastic hole. Thermoplastic molded parts and assemblies suitable for ultrasonic equipment Fast, repeatable installation can be suitable for production environments. Requires compatible ultrasonic equipment and carefully controlled force, vibration, and alignment. Not every plastic or part geometry is suitable.
Press-Fit or Knurled Inserts Pressed into a hole, typically at room temperature. Knurls, ribs, or other external features engage the surrounding material. Plastics, metals, and other materials, depending on insert design and hole preparation Simple installation with little or no heating; suitable designs can provide resistance to rotation. Retention depends on material, hole tolerance, wall thickness, and insert geometry. Excessive interference can crack or deform the workpiece.
Molded-In Inserts Positioned in a mold before the plastic is injected or formed around the insert. Injection-molded thermoplastics and some molded thermoset parts Integrates the threaded feature during part production and can provide strong mechanical anchoring. Requires insert placement and mold design. The insert must tolerate the molding process, and the surrounding material needs adequate support.
Self-Tapping Inserts Driven or screwed into a prepared hole. External cutting edges or forming features create or engage with the surrounding material. Selected plastics, wood, and soft metals, depending on insert design Can create a threaded attachment point without molding the insert into the part. Use the specified pilot-hole size and installation method. Cutting-style and thread-forming designs work differently and are not interchangeable in every material.
Expansion Inserts Installed in a prepared hole; a screw or installation tool expands part of the insert against the surrounding material. Some plastics, composites, wood, and other materials, depending on design Expansion can help secure the insert in a hole without a press-fit operation. Expansion force must be appropriate for the workpiece. Thin, brittle, or weak materials may split or deform if the hole or installation is unsuitable.
Rivet Nuts (Blind Threaded Inserts) Inserted into a pre-drilled hole and set with a hand or powered tool. The tool deforms the unthreaded portion behind the workpiece to clamp it in place. Sheet metal, thin panels, and some plastics or composites with suitable support Creates a threaded fastening point from one side of the workpiece, making it useful when the reverse side is difficult to access. Requires the correct grip range, hole size, and setting tool. Workpiece thickness and material affect joint strength and deformation risk.
Wire Thread Inserts A helical wire coil is screwed into a tapped parent-material hole using an installation tool; a tang, if present, may be removed afterward. Metal components with a prepared internal thread, including some thread-repair applications Can restore a damaged thread or provide a wear-resistant internal thread when properly specified. Requires a dedicated hole preparation and installation sequence. The correct tap, insert length, and installation depth are important.

Press-In, Heat-Set, and Ultrasonic Threaded Inserts

Press-in, heat-set, and ultrasonic inserts solve different problems in plastic parts. Press-in inserts rely on interference: ribs or knurls bite into a prepared hole as the insert is pushed into place. They suit tougher plastics and simple assembly lines, but hole diameter matters. A hole that is slightly oversized can reduce retention; one that is undersized may split a thin boss. Test samples from the actual resin lot, not just a CAD model.

Heat-set inserts soften the surrounding thermoplastic during installation, then lock in place as it cools. They work well in printed parts and molded components where repeated screw removal is expected. Ultrasonic inserts use vibration and pressure to melt a small area around the insert. TWI’s technical guidance on ultrasonic plastic joining identifies common operating frequencies of 20–40 kHz; that range helps explain why horn design and part support affect installation consistency. Small details matter. Neither process guarantees strong joints by itself. Resin, insert geometry, boss wall thickness, and installation settings all change pull-out performance. Record insertion force, torque-out, and pull-out results across several samples before choosing a method; the first test may look convincing, but it may not be repeatable.

Helical, Molded-In, and Self-Tapping Threaded Inserts

Helical inserts use a coiled metal wire to create durable internal threads in a prepared hole. They are often used to repair damaged threads or reinforce softer metal parts. Installation requires the correct drill size and a dedicated insertion tool. Fit matters. If the coil sits too high or too deep, the fastener may not seat properly.

Molded-in inserts are positioned inside a component mold before plastic is formed around them. Their knurls or other exterior features help resist rotation and pull-out. They can provide a strong fastening point in a plastic housing, especially where screws will be removed repeatedly. Placement needs care: a small shift during molding can leave the threaded opening off-center. Material shrinkage should also be considered during design.

Self-tapping inserts cut or form their own external thread as they are driven into a prepared hole. This can simplify assembly when there is no molded-in fastening point. A correctly sized pilot hole helps control installation force. Too much torque can crack brittle plastic or damage the insert’s internal threads. In practice, testing the chosen insert in the actual base material is worthwhile; similar-looking plastics can behave differently.

Threaded Insert Installation Features

The chart compares common installation characteristics: helical inserts are fitted into a prepared tapped hole, molded-in inserts are positioned during molding, and self-tapping inserts form or cut their mating thread in a pilot hole. Specific requirements vary by insert design and host material.

How to Select the Right Threaded Insert for an Application

How to Select the Right Threaded Insert for an Application

Selecting a threaded insert starts with the host material and the forces the joint must withstand. Soft plastics may need a heat-set or molded-in insert, while wood often suits a flanged insert with coarse external threads. For thin sheet metal, a press-in or rivet-style insert can provide a usable thread without access to both sides. Fit comes first.

Next, consider installation access, expected load, temperature, and how often the fastener will be removed. A helical insert can restore or reinforce a tapped metal hole, but it needs enough surrounding material and careful installation. Self-tapping inserts can work in plastics and softer materials, though their cutting action may split a thin wall. Check the manufacturer’s load data and installation dimensions rather than relying on appearance alone.

A practical trial helps. Install a sample in material matching the real part, then check for rotation, pull-out, and damage after tightening. Test it early. A small plastic boss may look sturdy on a drawing yet crack when the screw bottoms out. Leave clearance for the insert’s outer diameter and installation tool, and confirm the screw length will not press against hidden components. Even a careful choice may need revision when production materials or tolerances change.

Get a Quote
910-483-7828